






Description
-
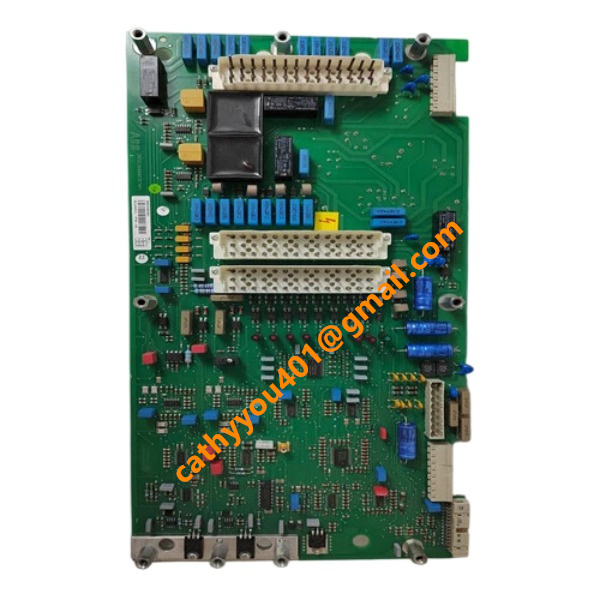
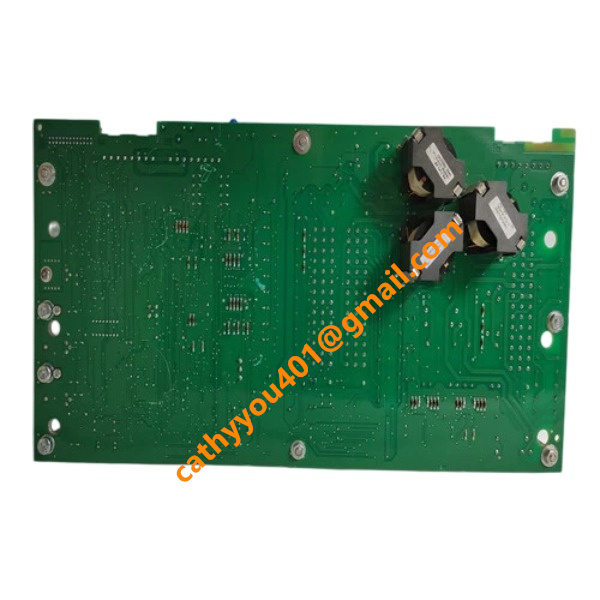
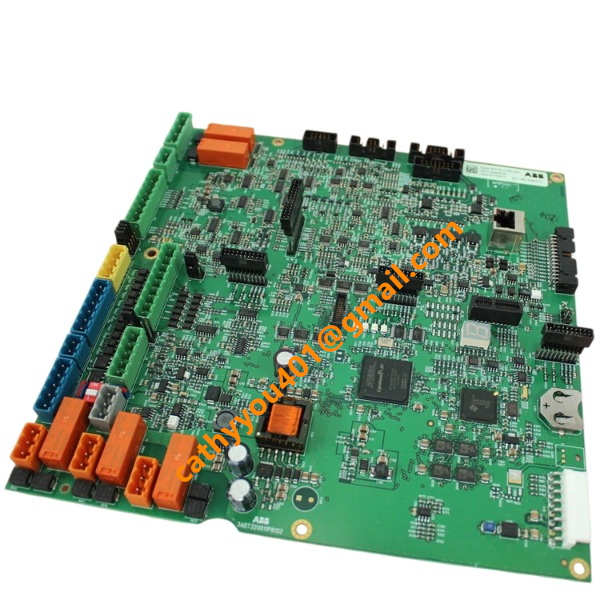
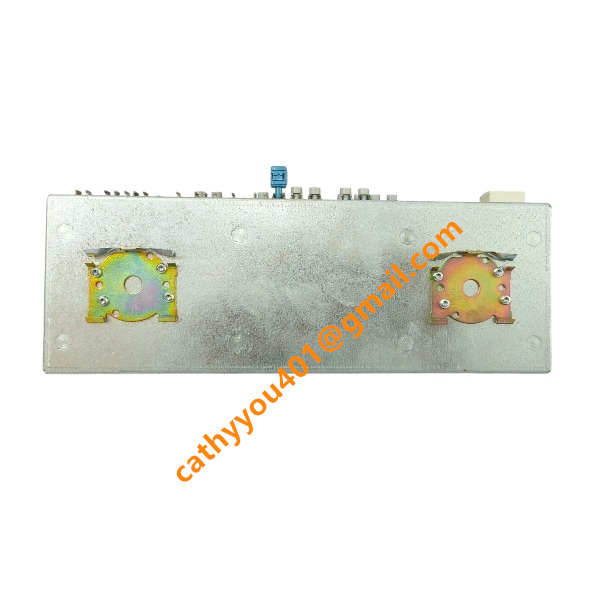
BrandABB
-
ModelPFSK142
-
Product NameAF100 Field Communication Control Board
-
Dimensions200 mm × 150 mm × 80 mm
-
Weight1.5 kg
-
Place of OriginSweden
-
HS Code85423190
-
Operating Temperature-25°C to +60°C
-
Storage Temperature-40°C to +85°C
-
Manufacturing part number3BSE006505R1
-
Warranty1 year
-
Statusnew brand
PFSK142 3BSE006505R1 ABB Technical Parameters
Product Type: Signal conditioning control board designed for ABB Advant Controller and S800 I/O system;
Power Supply: 24 V DC power supply supplied through the rack carrier;
Signal Conversion: Features 24-bit ADC and 14-bit /16-bit DAC channels to deliver high-precision analog signal processing;
Galvanic Isolation: Provides galvanic isolation between the field side and control system side to reduce electromagnetic interference;
Communication Interface: Supports AF100 fieldbus interface and Modbus RTU protocol for data communication with master controllers and field instruments;
Mounting Method: Installed on rack carrier;
Status Indication: Built-in on-board LED indicators to display power status, operating state and fault alarms;
Core Function: Acquires and conditions analog and digital field signals, sends processed data to the main control unit, receives control commands and outputs corresponding signals;
Diagnostic Function: Integrated self-diagnostic capability detects internal circuit failures, communication breaks and signal anomalies, and reports fault information to the controller;
Compatibility: Fully compatible with ABB Advant control platform and S800 I/O modules;
Signal Processing: Enables high-fidelity signal acquisition and conversion between field devices and DCS control systems.

PFSK142 3BSE006505R1 ABB Application Fields
Power generation industry: Deployed in turbine monitoring and generator excitation control systems. It delivers high-precision acquisition and isolation of shaft vibration, temperature and generator operating signals for the Advant DCS platform.
Oil & gas and petrochemical industry: Installed in distributed control systems for refineries and oilfields. It processes pressure, flow and temperature signals sourced from field transmitters and enables secure signal transmission within hazardous process zones.
Chemical industry: Applied to continuous process control in chemical plants. It carries out conditioning and conversion of analog and digital signals from reactors, separators and pipeline equipment to maintain stable closed-loop control.
Water treatment & wastewater industry: Used in automation systems for pumping stations and water treatment facilities to gather liquid level, flow and valve status signals and communicate with the main control system.
Metallurgy industry: Integrated into rolling mill and furnace control systems. It handles multiple field sensor signals to support real-time monitoring and interlock control of thermal and mechanical equipment.
General manufacturing automation: Suitable for production line control. It collects signals from sensors and actuators to coordinate the operation of motors, valves and conveying machinery.
Pharmaceutical industry: Utilized in pharmaceutical process control systems. It provides galvanic isolation and high-fidelity signal acquisition of process parameters within clean production environments.

GDB021BE
Unitrol 1020
698B275U01
SM810K01
BC810K02
PP886
PBA800
RED615


.jpg)